Heavy Engineering & Fabrication

Large fabricated components and assemblies, built at Oragadam, Chennai. Plate processing, fabrication, post-weld machining, finishing and inspection run on one route.
Build strategy
Plan the complete build before production
A large weldment has to be producible, movable, machinable, inspectable and installable. All five are decided on the drawing, not on the floor.
Technical review
Materials, tolerances, joint and weld access, and critical interfaces, checked before release.

Build sequence
Plate preparation, forming, fit-up, welding, handling, machining and finishing, sequenced as one route.

Datum & restraint plan
Datums and restraint points defined so alignment holds through the build.

Distortion & handling plan
Weld sequence, intermediate measurement, restraint and lifting method, all fixed before the first plate is cut.

Inspection hold points
Hold points placed where a correction is still practical.
Work packages
Components and assemblies
What we are set up to build at Oragadam.
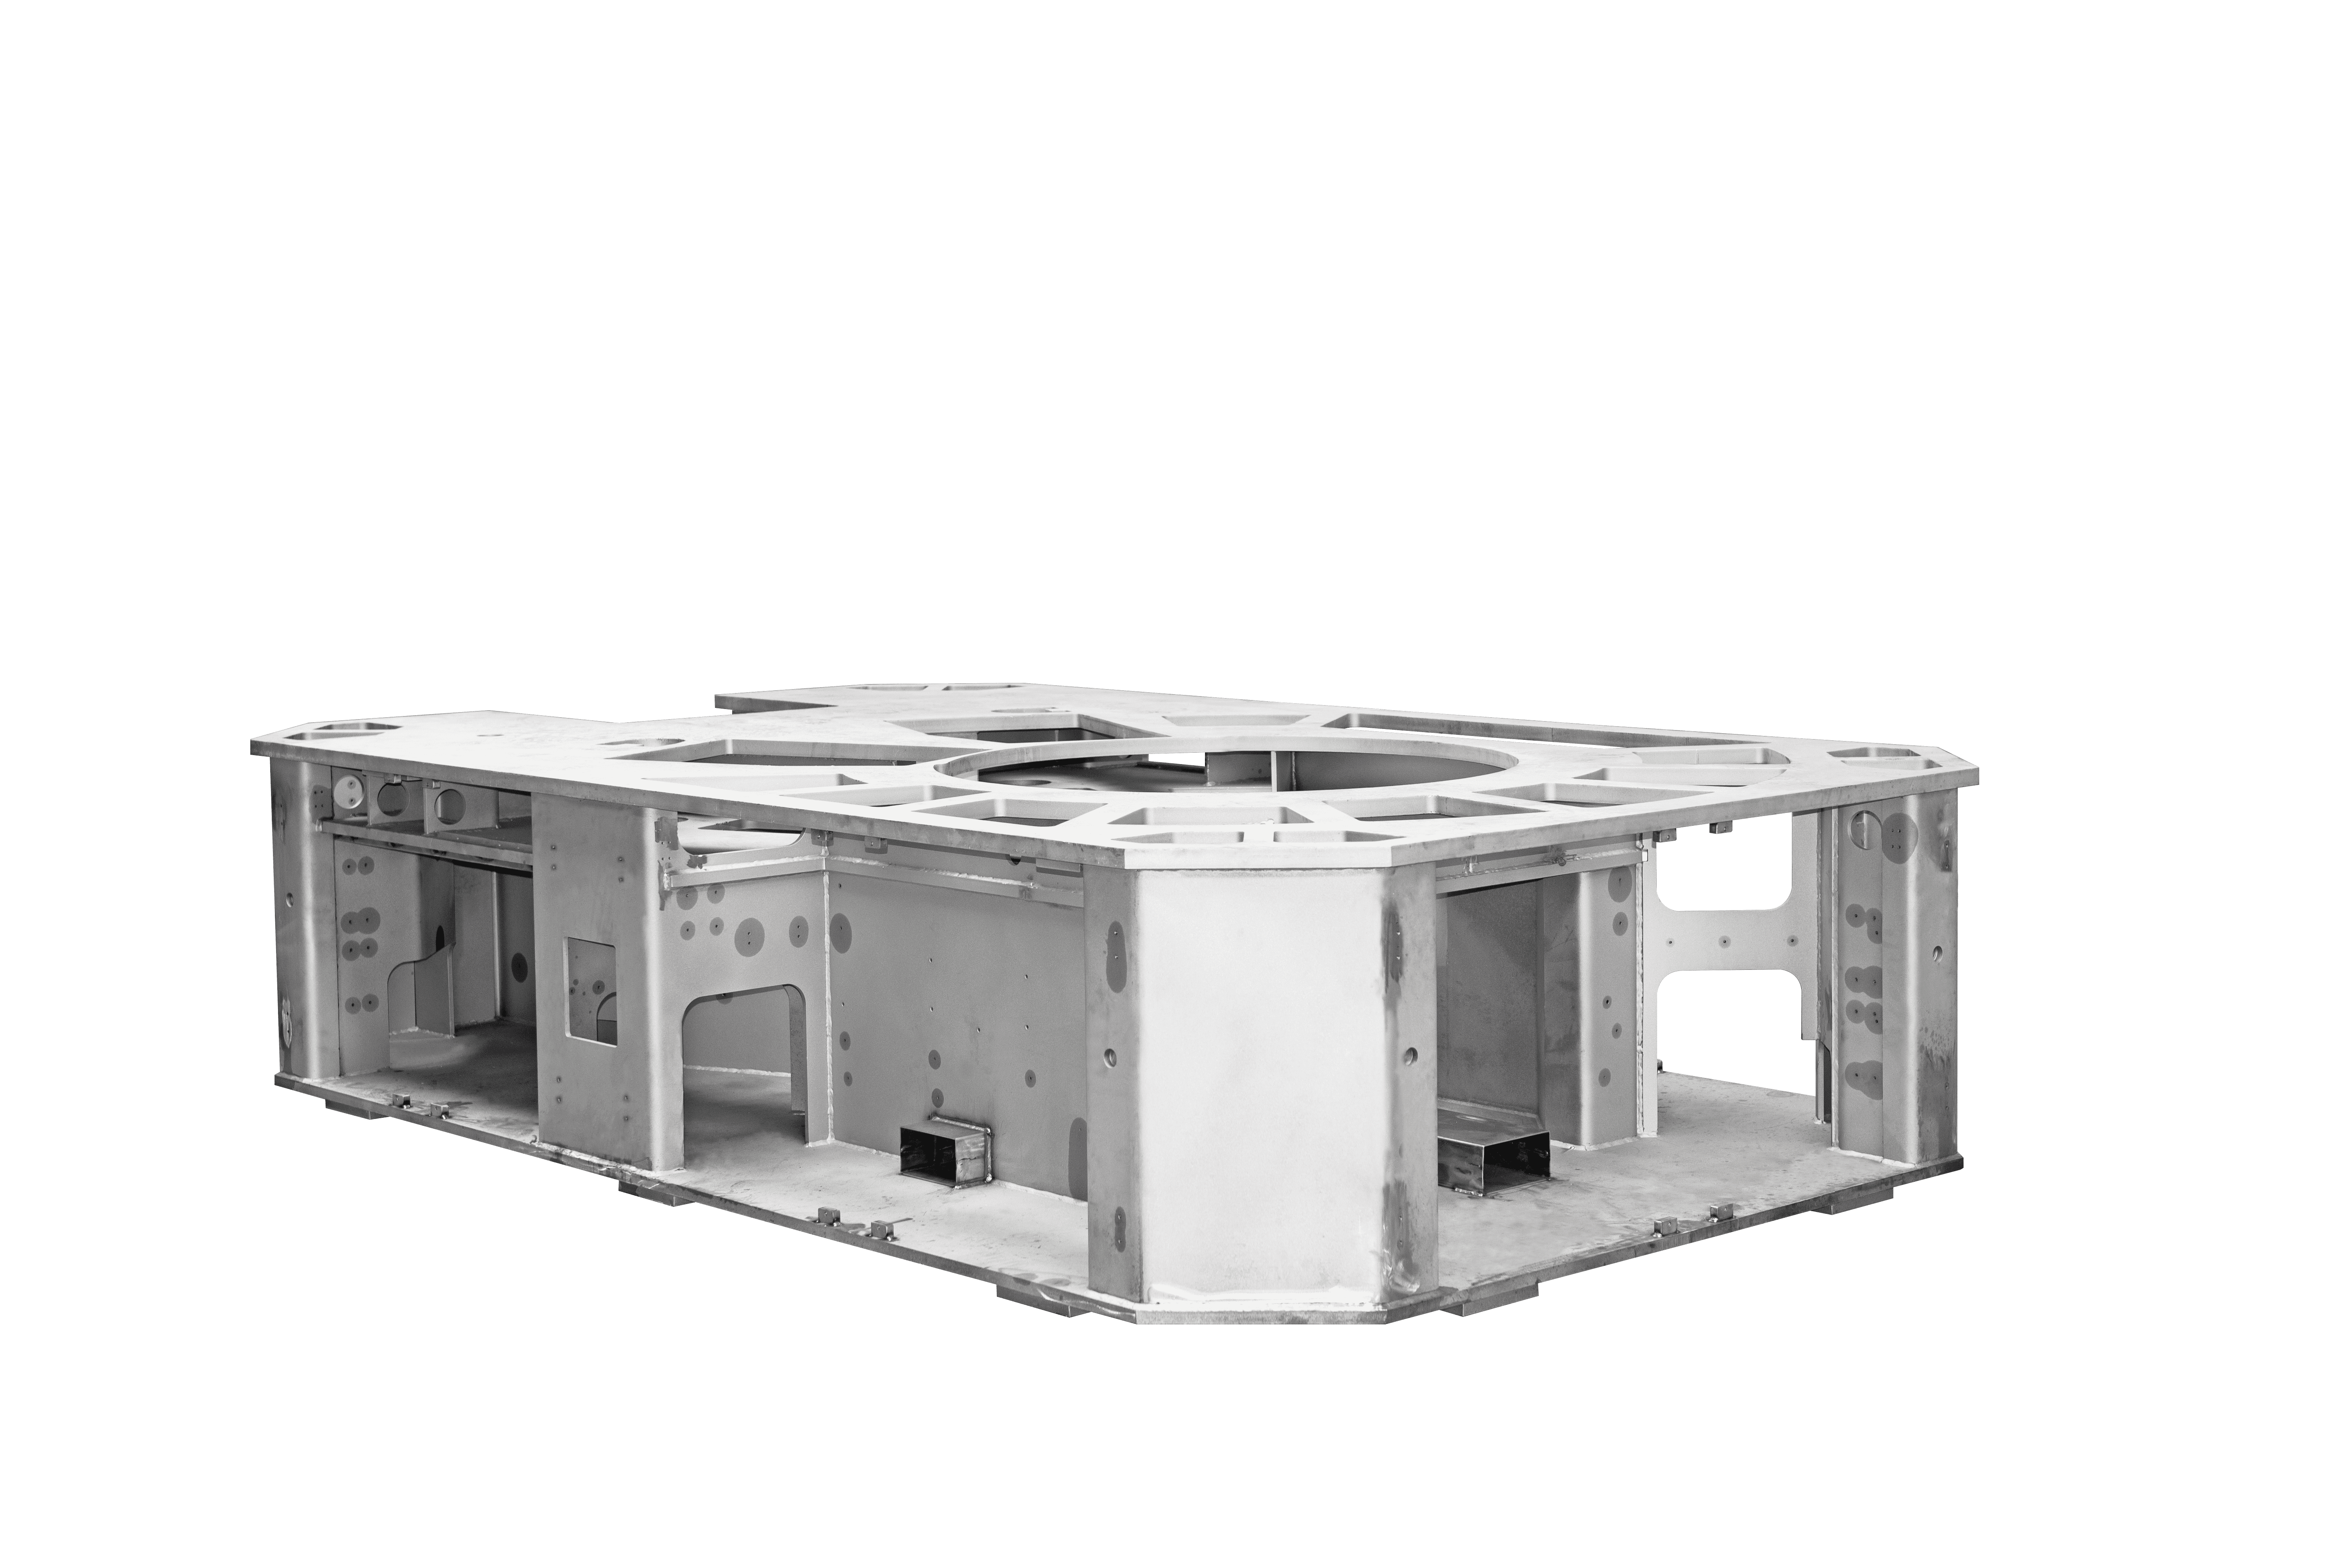 Machine bases & frames Weldments with machined mounting and alignment features. | 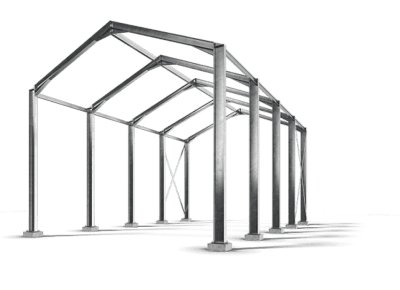 Structural frames & weldments Plate and section assemblies, delivered ready for integration. |
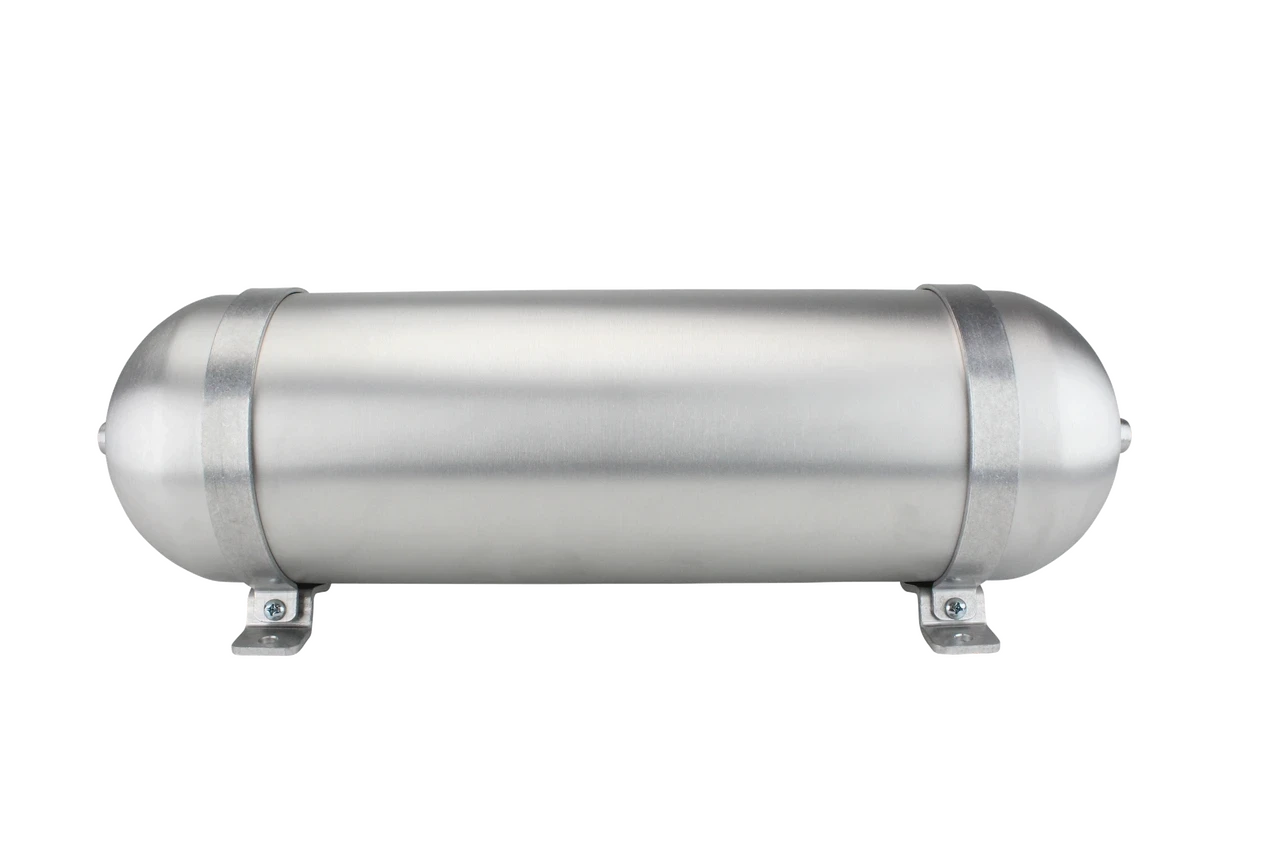 Tanks & enclosures Rolled and welded assemblies, coated to the agreed delivery condition. |  Construction & mining components Heavy plate parts and structures for heavy-duty equipment. |
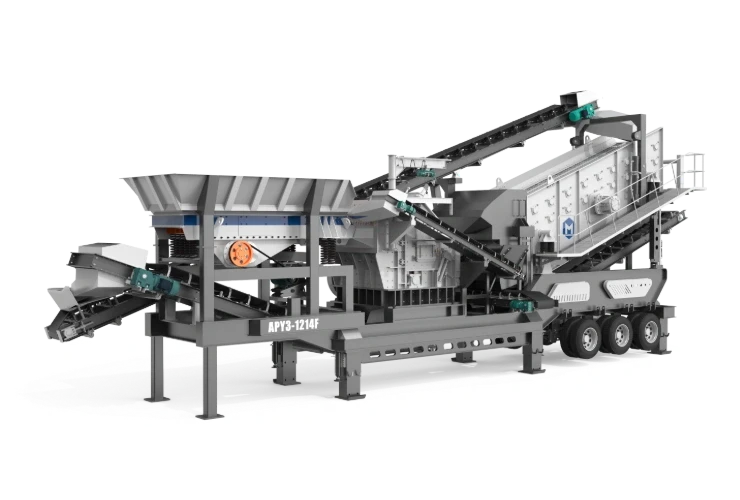 Crusher & crawler structures Large mobile-equipment weldments with controlled mounting interfaces. | 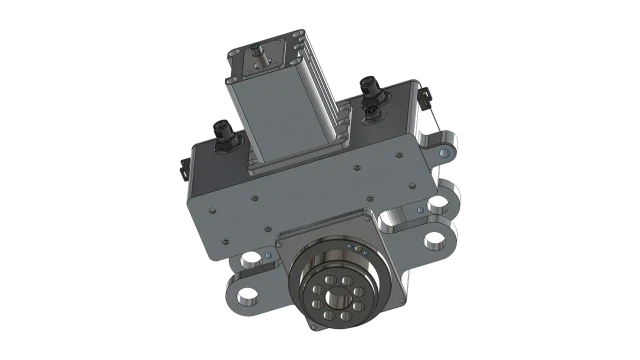 Fabricated subassemblies Multi-part builds delivered as one inspected assembly. |
Fit-up & welding

Control geometry through the build
Fit-up decides whether the finished interfaces line up. Heavy tables and purpose-built fixtures set the geometry. Weld sequence and in-process measurement keep it.
Fixture-controlled fit-up
Components located on heavy tables and purpose-built fixtures, against the defined datums.
MIG welding
Process planned around the material, the joint design and the volume.
In-process measurement
The planned weld sequence and restraint are followed, with geometry measured between stages.
Assembly responsibility
A multi-part fabrication stays one assembly, on one inspection route.
Plate processing
Controlled material preparation and accurate profiles
Cut quality, edge condition and formed geometry decide how fit-up and welding go. Large-format fibre-laser cutting, plate rolling and radial drilling produce consistent parts for fit-up.
Equipment and process capability
Equipment | Specification | Purpose |
|---|---|---|
Fibre laser | 20 kW, 8,150 × 2,540 mm | Large plate profiles |
Three-roll plate rolling machine | 100 tonne | Cylindrical and curved sections |
Radial drilling machines | RD-60 and RD-40 | Large workpieces and structural assemblies |
Edge & joint preparation | Set by the material and the welding procedure | Cutting and grinding to the required joint preparation |
Material handling | 14 t mobile; 5 t jib | Plate, work in progress and finished assemblies |
Post-weld machining

Machine critical interfaces against the defined datum strategy
Mounting faces, bearing locations, bores and hole patterns turn a weldment into a working assembly. The machining route is planned alongside the fabrication strategy, so datums, fixtures and handling stay aligned.
Vertical machining centres
Milling, drilling and finishing of critical interfaces.
Fourth-axis machining
Indexed and multi-face features in fewer setups, where the geometry allows it.
CNC turning
Rotational parts for fabricated assemblies.
Surface grinding
Flatness and surface finish where the drawing calls for it.
CAM & process planning
Tooling, workholding and operation sequence planned as one route.
Finishing

Finish to the agreed delivery condition
Preparation and coating are chosen for the service environment, the coating specification and your acceptance criteria.
Grinding & dressing
Weld finishing, edge treatment and local preparation.
Shot blasting
Cleaning and surface preparation before coating.
Wet painting
Applied to fabricated structures and assemblies.
Powder coating
Applied in Chennai, for suitable parts and specifications.
Final preparation
Cleaned, protected and staged for inspection and dispatch.
Next step
Send the drawing, material, tolerances and quantity.
We quote heavy fabrication, post-weld machining, surface preparation, inspection and documented delivery as one scope, and tell you what else we need.
Capabilities


